

Why Industrial Epoxy Floor Coating is the Gold Standard for Durability
Industrial epoxy floor coating provides best durability and chemical resistance for demanding commercial and manufacturing environments. These high-performance systems range from 10-250 mils thick – up to 10 times thicker than standard floor paint – and can withstand heavy forklift traffic, chemical spills, and extreme temperatures for 10+ years.
Key Benefits of Industrial Epoxy Floor Coatings:
- Thickness: 10-250 mils vs. 3 mils for standard paint
- Durability: 10+ year lifespan with proper installation
- Chemical Resistance: Withstands acids, oils, and cleaning agents
- Seamless Surface: Prevents bacteria growth and simplifies cleaning
- Heavy Traffic Ready: Handles forklifts, equipment, and high foot traffic
- Cost Range: $3-30 per square foot depending on system complexity
Whether you’re upgrading a warehouse floor, food processing facility, or aircraft hangar, the right industrial coating system eliminates costly downtime from repairs and refinishing.
I’m Mike Wislinsky, founder of Denver Floor Coatings with over 20 years of engineering and operations experience at 3M, where I led teams implementing industrial epoxy floor coating solutions across multiple manufacturing facilities.
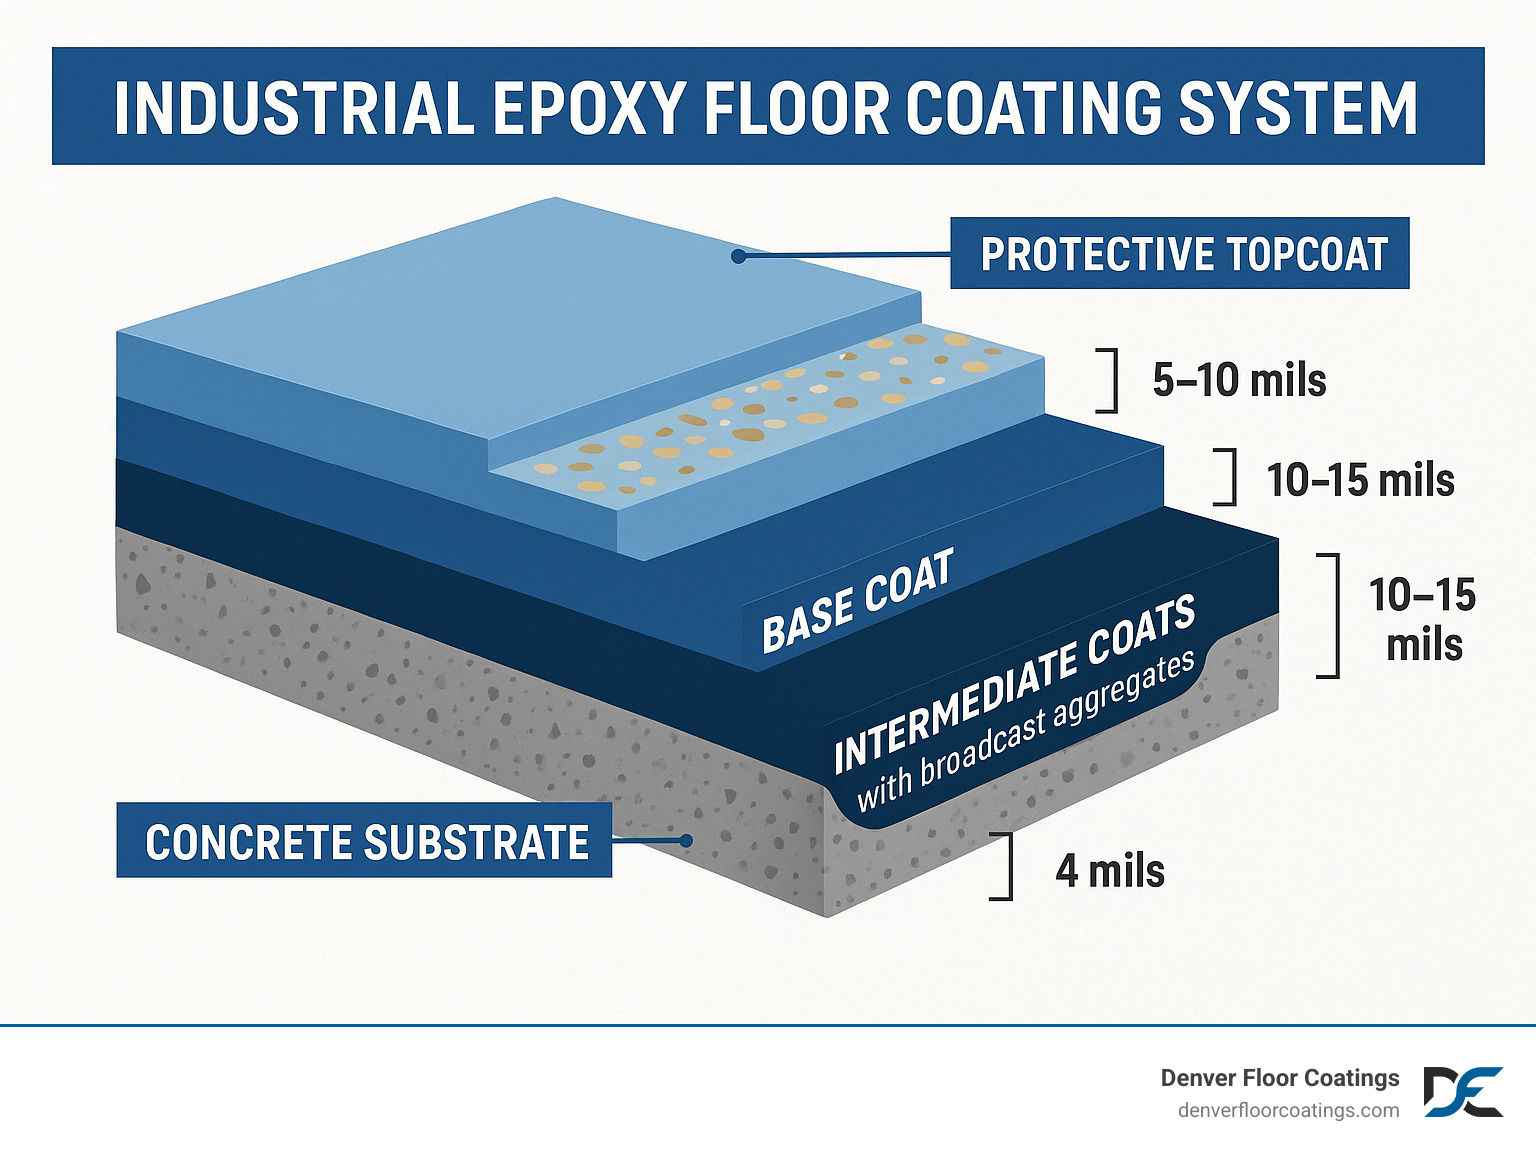
Industrial Epoxy Floor Coating 101
When you walk across a perfectly smooth warehouse floor that’s been handling heavy equipment for years without a scratch, you’re experiencing the power of industrial epoxy floor coating chemistry. Unlike regular paint that just sits on top of concrete, epoxy creates something entirely different through a fascinating two-part chemical reaction.
When you mix the resin and hardener components, they undergo a chemical change called cross-linking. This cross-linked polymer doesn’t just coat your concrete – it actually bonds with it at the molecular level, becoming part of the floor itself.
The chemistry gets even more impressive when you consider that most industrial systems use 100% solids epoxy formulations. This means there are no solvents that evaporate during curing, resulting in zero or very low VOC emissions.
The thickness range for these systems spans from 10 mils for lighter-duty applications all the way up to 250 mils for the most demanding environments. To put that in perspective, regular floor paint cures at only 3 mils. That dramatic difference in thickness translates directly into years of additional service life.
Industries from food processing to aerospace manufacturing rely on these coating systems because they can be customized with different chemistries, aggregates, and specialized additives.
What Sets an Industrial Epoxy Floor Coating Apart from Paint?
The difference between industrial epoxy floor coating and regular floor paint is like comparing a suspension bridge to a rope bridge – the engineering is completely different.
Paint forms a decorative film that sits on your concrete surface, relying on mechanical adhesion. When that grip fails, the paint starts peeling and chipping away.
Epoxy works through chemical adhesion, which is far more powerful. It actually penetrates into the concrete pores and forms millions of chemical bonds with the substrate. This creates a cross-link density that’s exponentially stronger than paint’s simple mechanical grip.
The thickness advantage is equally dramatic. While paint gives you 3 mils of protection, industrial epoxy systems deliver 10-250 mils of armor for your floor. Properly formulated epoxy systems can handle substrate movement, flexing with concrete expansion and contraction while maintaining their protective seal. That’s why you’ll see 10+ year lifespans from industrial epoxy installations versus the 1-2 years from painted floors.
Key Environments for Industrial Epoxy Floor Coating
Food processing facilities represent the ultimate test for any floor coating system. These environments demand surfaces that can handle daily washdowns with scalding water and aggressive sanitizing chemicals, all while maintaining a seamless, hygienic surface that won’t harbor bacteria.
Aircraft hangars need floors that can support massive point loads from landing gear while shrugging off hydraulic fluid spills, jet fuel, and harsh de-icing chemicals. The seamless nature of industrial epoxy floor coating eliminates joints where contaminants could collect.
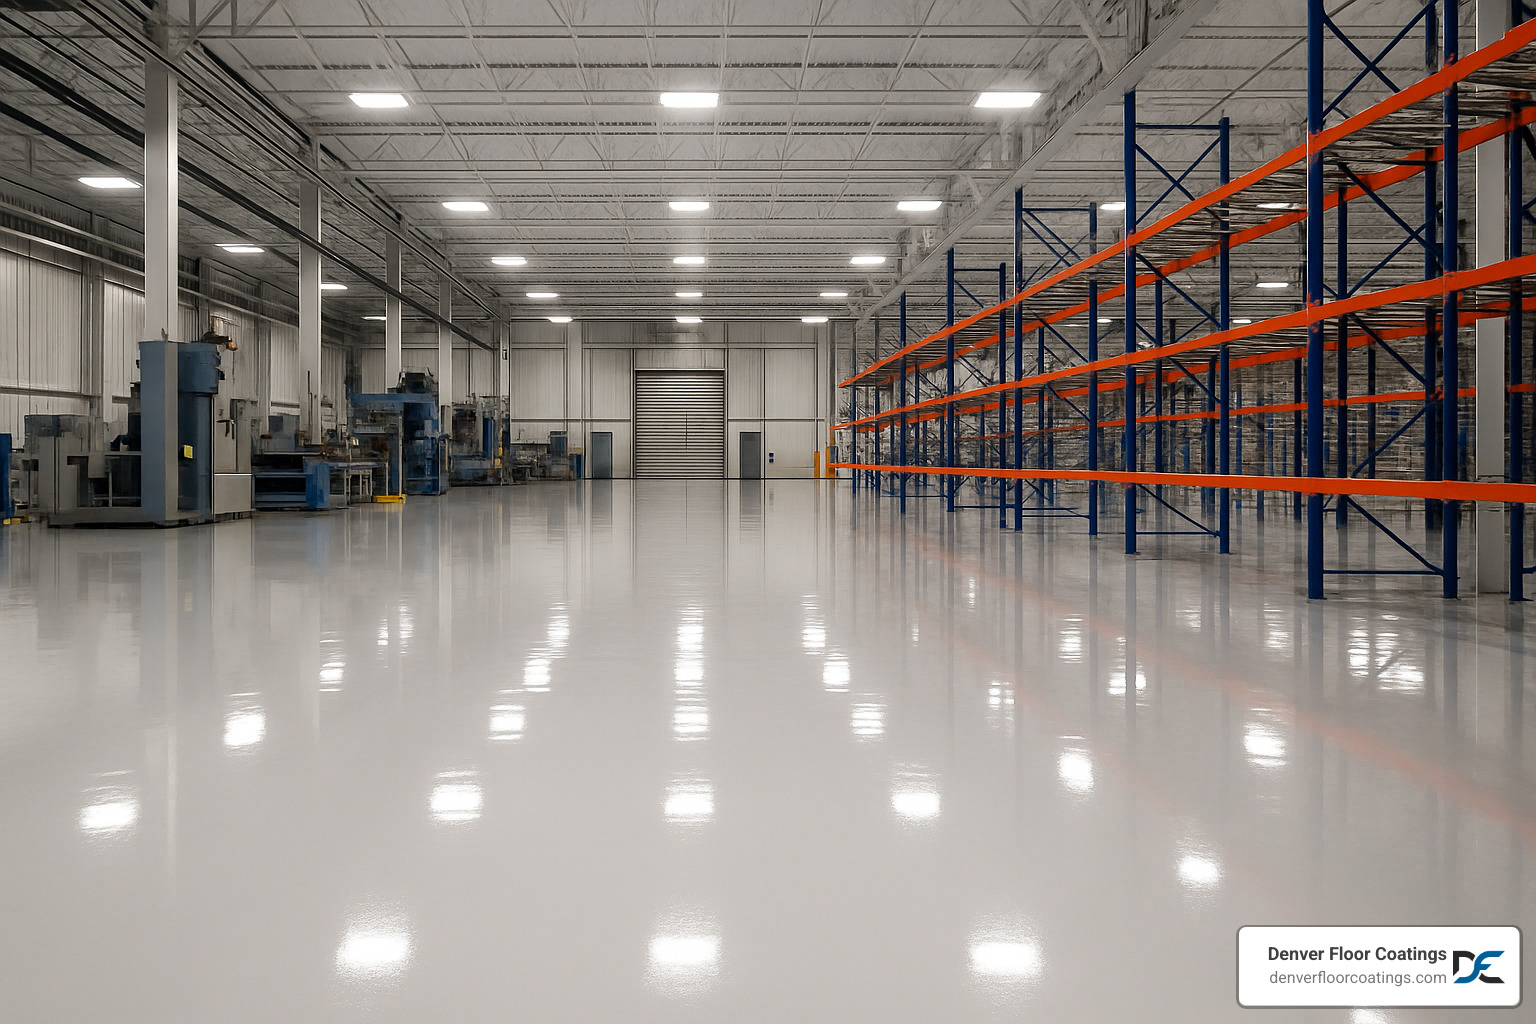
Warehouses and distribution centers subject their floors to relentless punishment from forklift traffic and heavy equipment loads. Industrial epoxy systems provide the durability needed to maintain smooth, safe surfaces under these conditions while their light reflectivity can reduce lighting costs.
Clean rooms in pharmaceutical and medical device manufacturing demand ultra-smooth, seamless surfaces that won’t generate particles or harbor contaminants. Self-leveling epoxy systems create the mirror-like finishes these controlled environments require.
Benefits & Performance Metrics
When you’re investing in an industrial epoxy floor coating system, the performance advantages are measurable differences that directly impact your bottom line through reduced maintenance costs and extended floor life.
Abrasion resistance is where industrial epoxy really shines. Premium industrial epoxy systems achieve ratings as low as 4mg of material loss in Taber Abrasion Tests – compared to 24-55mg for standard commercial epoxies. This means your floor will look good and perform well years longer under heavy forklift traffic.
Chemical resistance varies by formulation, but even standard systems handle most oils, cleaning agents, and mild acids without breaking down. Specialized novolac epoxies can resist concentrated acids and caustics that would destroy other flooring materials, preventing costly substrate damage.
The impact strength of thick epoxy systems is remarkable. That 10-250 mil thickness creates a flexible polymer structure that absorbs and distributes force from dropped tools, equipment impacts, and heavy wheeled traffic. Instead of cracking like thin coatings, industrial epoxy bounces back.
Light reflectivity from high-gloss epoxy finishes can improve facility lighting by 30% or more, translating to real energy savings while making workplaces safer through better visibility.
The hygienic properties of seamless epoxy surfaces eliminate grout lines and joints where bacteria hide. You can thoroughly clean and sanitize with standard procedures, which is why epoxy dominates in food processing, healthcare, and pharmaceutical facilities.
Safety Upgrades & Slip Control
Safety isn’t negotiable in industrial environments, and modern industrial epoxy floor coating systems give you multiple ways to control slip hazards. The key is finding the balance between traction and cleanability.
Anti-slip aggregates can be broadcast into the coating during application, creating controlled texture that maintains grip even when surfaces get wet. Options include aluminum oxide for aggressive texture, silica sand for moderate slip resistance, and specialized polymer beads that provide excellent traction while staying easy to clean.
OSHA compliance requirements vary by industry, but properly designed epoxy systems can meet or exceed required coefficient of friction standards. The ability to customize slip resistance during installation makes epoxy ideal for facilities with varying conditions throughout different work areas.

Longevity Factors & Wear Testing
That 10+ year lifespan typical of industrial epoxy floor coating systems depends on getting the fundamentals right from day one.
Substrate preparation is absolutely critical. Surface profiling through diamond grinding or shotblasting creates the mechanical bond necessary for long-term adhesion. Moisture testing ensures your concrete is ready for coating – applying epoxy over damp concrete causes failure.
Traffic loads must be accurately assessed during system design. Underestimating traffic loads is one of the most common causes of premature coating failure.
The abrasion loss rating of 4mg achieved by premium systems demonstrates why chemistry and thickness matter in wear resistance. This superior performance comes from 100% solids formulations and optimal cross-link density achieved through proper mixing and curing.
Installation & Thickness Essentials
Getting an industrial epoxy floor coating right isn’t just about mixing resin and hardener – every step in the installation process affects final performance. Proper installation makes the difference between a floor that lasts 10+ years and one that fails within months.
Surface preparation takes about 70% of installation time. Moisture testing using calcium chloride tests identifies potential problems before they become expensive failures. Surface profiling through diamond grinding or shotblasting removes contaminants while creating 2-4 mils deep texture for mechanical bonding.
Crack repair gets handled before any coating application. Primer selection depends on substrate conditions, moisture levels, and the specific epoxy system. Build coats and intermediate layers create the thickness and performance needed, often including broadcast aggregates for texture and additional thickness.
The topcoat affects both appearance and performance. Cure times typically run 6-24 hours between coats and 48-72 hours before full traffic loading.
More info about professional installation
Surface Preparation Checklist
Diamond grinding creates uniform profile while removing surface contaminants in one step. Shotblasting works well for larger areas and handles more aggressive surface preparation needs.
ASTM standards provide the roadmap for consistent results, including ASTM D4259 for abrasion testing and ASTM F1869 for moisture vapor emission testing.
Vapor barrier systems become necessary when moisture vapor emission rates exceed what coating systems can handle.
Optimal Thickness for Industrial Epoxy Floor Coating Systems
The relationship between coating thickness and performance is straightforward – more thickness generally means better performance, but also higher cost.
Coatings at 10-30 mils thick provide excellent chemical resistance and moderate wear resistance, perfect for light to moderate traffic applications.
Slurries ranging from 30-125 mils incorporate fine aggregates that boost thickness and impact resistance while keeping surfaces relatively smooth. These handle moderate to heavy traffic areas with regular forklift traffic.
Mortars at 125-250+ mils thick use larger aggregates and can be trowel-applied to create extremely durable surfaces that withstand the heaviest traffic and impact conditions.

Product Roundup: Epoxy Systems That Last
When it comes to industrial epoxy floor coating systems, there’s no one-size-fits-all solution. The beauty of modern epoxy technology lies in having the right system for every industrial challenge.
High-Build 100% Solids Coatings
These are the workhorses of industrial flooring. At 25 mils thick, high-build 100% solids coatings deliver serious durability with a beautiful high-gloss finish.
The “100% solids” means every bit of material you apply stays put. No solvents evaporating away, no shrinkage, just solid protection. This is why these systems can handle heavy forklift traffic day after day without showing wear.
These systems offer quick turnaround time. Most installations can be completed over a weekend, so your facility is back to full operation by Monday morning.
The high-gloss finish reflects light throughout your space, which can cut lighting costs while making the work environment brighter and safer.
Self-Leveling & Decorative Formulations
Self-leveling systems literally flow and level themselves to create surfaces so smooth they look like glass. Clean rooms and laboratories love these systems because there’s nowhere for contaminants to hide.
Decorative doesn’t mean delicate. Modern self-leveling systems can incorporate metallic pigments that create stunning visual effects while maintaining full industrial performance.
You can also add decorative flakes or quartz broadcast during installation to create custom looks that match your company’s branding.
Novolac & Specialty Chem-Resist Options
When standard epoxy isn’t tough enough, novolac systems are the heavy-duty champions of chemical resistance, built to handle acids, caustics, and high temperatures that would destroy regular coatings.
The molecular structure creates such a tightly cross-linked barrier that aggressive chemicals simply can’t penetrate. This makes them essential for chemical processing facilities, laboratories, and any operation where spills are inevitable.
High-temperature resistance is another advantage of novolac systems. While standard epoxies might soften when exposed to heat from industrial processes, novolac systems maintain their integrity and protection.
Maintenance, Costs & ROI
The real-world benefits of industrial epoxy floor coating systems tell a compelling story that goes far beyond initial installation cost.
Epoxy floors are refreshingly simple for daily care: regular cleaning with pH-neutral detergents and occasional degreasing when needed. No special waxing, no periodic refinishing, no replacement of damaged sections.
The seamless surface eliminates grout lines, joints, or seams where spills, dirt, or bacteria can hide. This makes thorough cleaning easy – a game-changer for food processing facilities requiring USDA compliance or healthcare environments where contamination control is critical.
Properly installed industrial epoxy floor coating systems typically deliver 10+ years of reliable service. When you factor in dramatically reduced maintenance costs over that decade-plus lifespan, most facilities see positive ROI within just 2-3 years through reduced cleaning time, eliminated floor repairs, and extended service intervals.
One valuable benefit often gets overlooked: downtime savings. Many epoxy installations can be completed over a weekend, allowing normal operations to resume Monday morning. The operational disruption savings alone can justify the investment.
More info about How to Clean Epoxy Floors

Frequently Asked Questions about Industrial Epoxy Floor Coating
How long does an epoxy floor last in industrial use?
Here’s the honest answer: a properly installed industrial epoxy floor coating system will typically serve you well for 10-15 years, sometimes even longer. But like most things in life, it depends on how hard you’re working it.
I’ve seen light industrial facilities with minimal chemical exposure get 15+ years from their floors. These are the lucky ones – maybe a warehouse with occasional forklift traffic or a clean manufacturing environment. On the flip side, heavy-duty operations with constant equipment traffic and aggressive chemical exposure might need to refresh their floors every 8-10 years.
The secret sauce? Accurate assessment during the design phase. Most premature failures happen because someone underestimated the beating the floor would take. Traffic loads, chemical spills, temperature swings – we need to account for all of it upfront.
Think of it this way: if you tell us your floor will see light use but then run heavy forklifts over it daily, even the best coating won’t last as long as expected. Honesty during planning saves headaches later.
Can coatings be applied over damaged or old epoxy?
Absolutely! Most industrial epoxy floor coating systems can go right over existing epoxy floors. It’s like giving your floor a fresh start without starting from scratch.
The catch? The existing coating needs to be well-bonded and properly prepared. We’ll thoroughly clean the surface and lightly abrade it to create the mechanical bond the new system needs. Think of it as roughing up the surface so the new coating has something to grip onto.
Damaged areas need attention first. Small cracks and chips? No problem – we fill those with compatible repair materials. Larger areas where the coating is peeling or delaminated? Those sections need to come off so we can properly prepare the substrate underneath.
Here’s where experience matters: compatibility between the old and new systems is crucial. Some chemical combinations just don’t play well together and can cause adhesion problems down the road. That’s why we always assess the existing coating before recommending a recoating approach.
Are epoxy floors slippery when wet?
Standard smooth epoxy floors can indeed become slippery when wet – but this is completely preventable with proper system design. Nobody wants a beautiful floor that becomes a safety hazard the moment someone spills a drink.
Anti-slip additives are the solution. We can incorporate these during application to create controlled texture that maintains traction even when wet. It’s like adding grip tape, but integrated right into the coating itself.
The beauty is in the customization. Need light texture for easy cleaning? We’ve got you covered. Need aggressive texture for maximum slip resistance in areas prone to spills? We can do that too. The level of slip resistance can be custom to meet specific OSHA requirements or your facility’s safety standards.
Modern anti-slip systems strike the perfect balance between safety and cleanability. You get the traction needed for safe operations without creating a textured surface that traps dirt and becomes impossible to clean. It’s industrial-strength safety that doesn’t compromise on maintenance.
Conclusion
When you’re running a manufacturing facility, warehouse, or food processing plant, your floor is critical infrastructure that affects everything from safety to productivity. Industrial epoxy floor coating systems deliver the durability, chemical resistance, and longevity that demanding environments require, with service lives exceeding 10 years and thickness options from 10-250 mils.
At Denver Floor Coatings, we understand industrial environments through over 20 years of engineering and operations experience at 3M. We don’t just spray coating on your floor – we engineer solutions based on your specific traffic loads, chemical exposures, and operational requirements.
Our single-day installation approach means your operations keep running while we transform your floors. Most installations are completed over a weekend, so you’re back to full production Monday morning with a floor system that will serve you for the next decade or more.
The math is simple: reduced maintenance costs, eliminated downtime from floor repairs, improved safety, and improved light reflectivity that can cut energy costs. Industrial epoxy floor coating systems pay for themselves through operational improvements while protecting your concrete substrate from damage that would cost thousands to repair.
Ready to upgrade your facility with flooring that actually works as hard as you do? Let’s talk about your specific challenges and design a coating system that delivers the performance your operation demands.