

Why Industrial Floor Coatings Are Essential for Modern Facilities
Industrial floor coatings are specialized protective systems designed to shield concrete floors from heavy traffic, chemical spills, and harsh environmental conditions. These high-performance coatings create seamless, durable surfaces that can withstand the demanding requirements of warehouses, manufacturing plants, food processing facilities, and commercial kitchens.
Top industrial floor coating types include:
- Epoxy systems – Chemical resistant, 7-250 mils thick, ideal for moderate traffic
- Polyurethane topcoats – UV stable, flexible, excellent for outdoor exposure
- Polyaspartic coatings – Fast cure (6 hours), temperature tolerant, minimal downtime
- MMA (Methyl Methacrylate) – Rapid cure, extreme temperature range, high traffic
- Urethane cement – Thermal shock resistant, hygienic, food-grade applications
- Anti-static (ESD) – Electrostatic discharge protection for electronics/labs
- Acrylic sealers – Basic protection, economical, light-duty applications
Modern industrial facilities face constant challenges from forklift traffic, chemical exposure, temperature fluctuations, and regulatory compliance requirements. The right coating system protects your concrete investment while ensuring worker safety and operational efficiency.
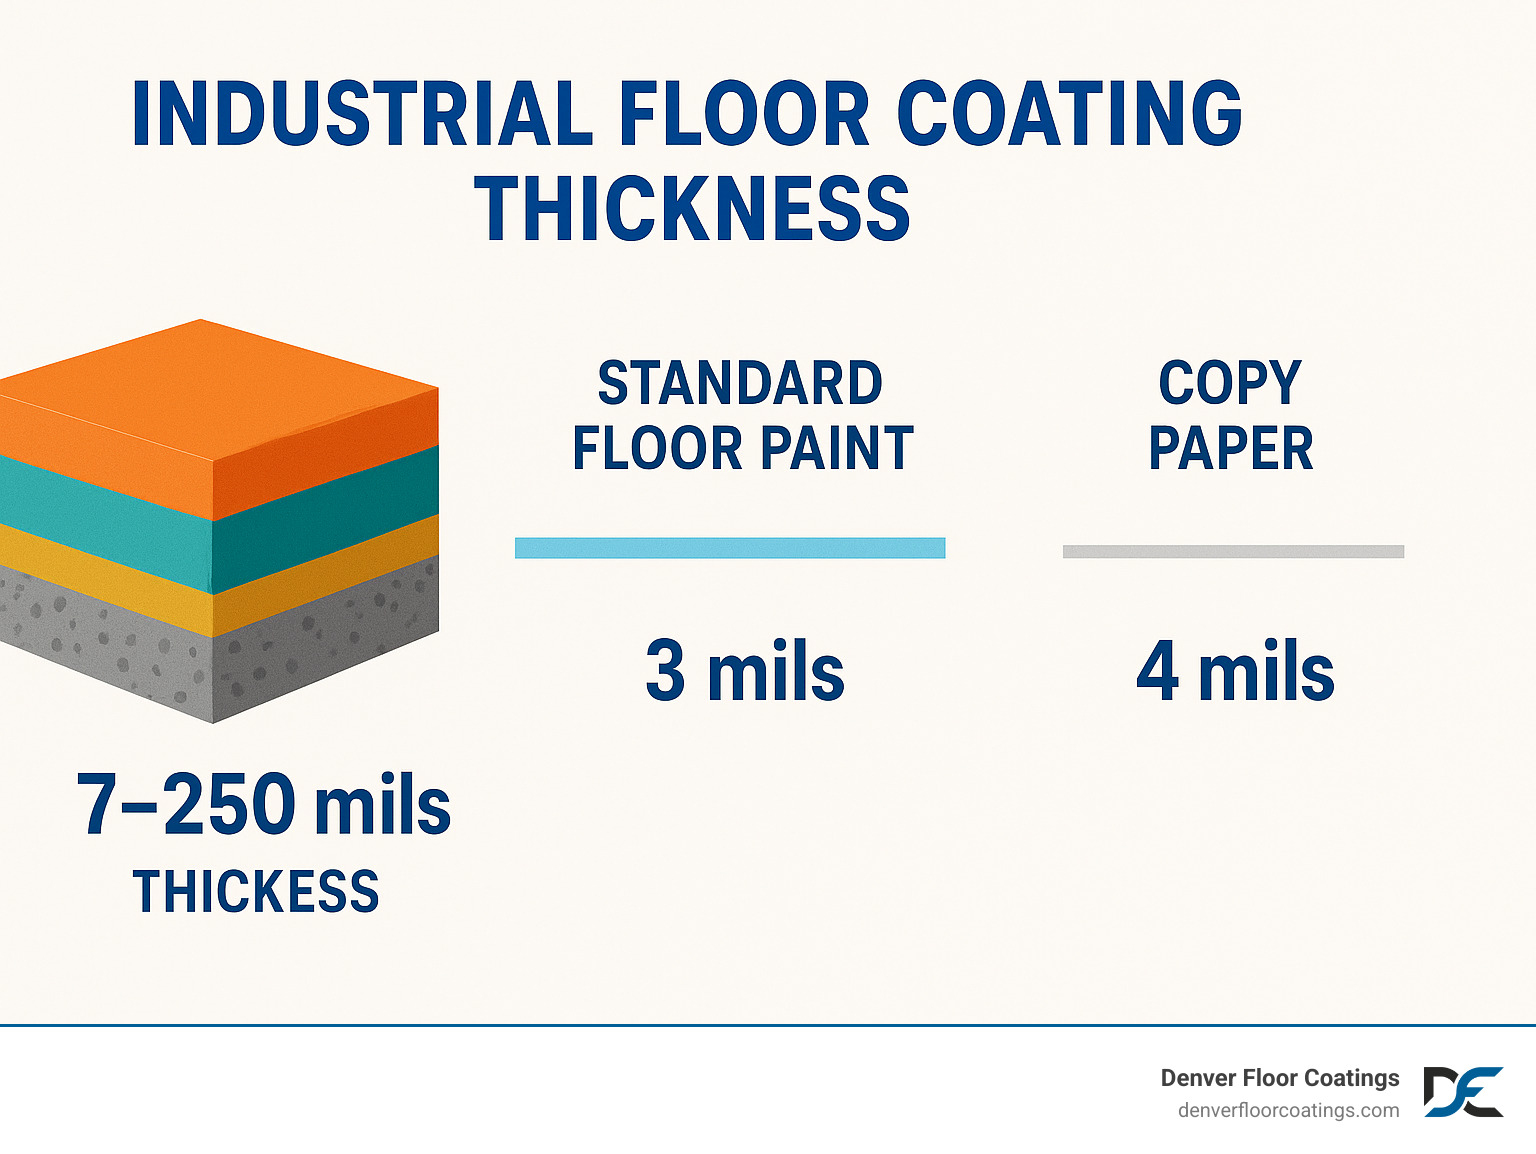
These coatings range from 7 to 250 mils in thickness – dramatically thicker than standard floor paints that cure at just 3 mils. This substantial build provides the durability needed for industrial environments while offering benefits like slip resistance, easy cleaning, and improved indoor air quality through low-VOC formulations.
I’m Mike Wislinsky, Founder and President of Denver Floor Coatings, with over 20 years of experience in engineering and operations management at 3M, where I led teams implementing industrial floor coatings across multiple manufacturing facilities. My expertise in process improvements and quality improvements has given me deep insight into what makes coating systems succeed or fail in demanding industrial environments.
Industrial Floor Coatings 101: What & Why
Think of industrial floor coatings as the armor your concrete floors desperately need. While concrete might seem tough, it’s actually quite vulnerable – full of tiny pores that soak up spills, chemicals, and moisture like a sponge. Without proper protection, those concrete floors can quickly turn into cracked, stained, and potentially unsafe surfaces.
These specialized coating systems go way beyond slapping some paint on the floor. We’re talking about engineered solutions that create a protective barrier between your concrete and whatever punishment your facility dishes out daily.
Substrate protection forms the foundation of why these coatings matter so much. Concrete handles compression well, but it’s surprisingly defenseless against chemical attacks, moisture penetration, and surface wear. Once damage starts, it spreads fast.
Regulatory compliance often drives the coating conversation. OSHA standards demand slip-resistant surfaces and proper chemical containment. USDA and FDA requirements get even stricter for food processing facilities, mandating seamless surfaces that can be easily sanitized. And if you’re working with sensitive electronics, ESD control becomes absolutely critical.
Indoor air quality has become a huge factor in coating selection. With people spending over 80% of their time indoors according to the Environmental Protection Agency, low-VOC formulations aren’t just nice to have – they’re essential for creating healthier work environments.
Key Benefits of Industrial Floor Coatings
Chemical resistance takes center stage when evaluating coating performance. Industrial facilities face a daily assault from acids, bases, solvents, oils, and aggressive cleaning chemicals. The right coating creates an impermeable shield that protects against chemical spills that would otherwise damage unprotected concrete.
Abrasion resistance protects against the constant grinding of foot traffic, wheeled equipment, and material handling. High-performance systems can achieve abrasion loss ratings as low as 4mg – dramatically better than typical commercial coatings that rate between 24-55mg.
When heavy objects get dropped or dragged across your floors, impact resistance prevents the cracking and chipping that can quickly spiral into major floor damage. This becomes especially important in warehouses and manufacturing facilities.
Hygiene benefits shine in facilities where cleanliness isn’t optional. Seamless surfaces eliminate the cracks and crevices where dirt and bacteria love to hide. Easy cleaning and sanitization become possible, while resistance to staining and odor absorption keeps facilities looking and smelling professional.
Slip resistance addresses one of the leading causes of workplace injuries while maintaining easy-clean benefits. Through specialized texture additives and topcoats, coatings can be engineered to provide the exact level of slip resistance your specific application demands.
Side-by-Side Comparison of Top Coating Types
Choosing the right industrial floor coating feels a bit like picking the perfect tool for a job – each chemistry has its sweet spot where it truly shines.
Epoxy systems are the reliable workhorses of industrial flooring. These systems build up from 7 to 250 mils thick and handle acids, bases, and solvents that would damage unprotected concrete. The catch? They don’t love UV light and can get cranky in extreme cold.
Polyurethane topcoats are the sun-lovers of the coating world. While epoxy hides from UV rays, polyurethane soaks them up without fading. These coatings stay flexible when temperatures swing wildly, making them perfect for areas with skylights or loading dock doors.
Polyaspartic coatings have completely changed the game for facilities that can’t afford downtime. Six hours from application to forklift traffic – these speed demons cure faster than you can finish your paperwork, all while delivering excellent UV stability.
MMA (Methyl Methacrylate) systems are the arctic explorers of industrial coatings. Sub-zero temperatures that stop other coatings cold? MMA just keeps curing. These systems create incredibly durable surfaces that handle the heaviest traffic for decades.
Urethane cement systems were practically designed for food processing plants. They combine urethane’s chemical resistance with cement’s ability to handle thermal shock. Hot sanitizer washdowns that would stress other coatings are just another day at the office for urethane cement.
Anti-static (ESD) coatings serve a critical role – safely channeling electrical charges away from sensitive equipment or flammable materials. Electronics manufacturing, laboratories, and chemical processing facilities rely on these specialized systems.
Acrylic sealers are the budget-friendly option for light-duty applications. They won’t win any durability contests, but they provide decent protection for low-traffic areas without the investment required for high-performance systems.

Pros & Cons of Industrial Floor Coatings
Epoxy systems deliver solid 10 to 20-year lifespans when properly matched to their application. They’re ready for foot traffic overnight but need 72 hours before heavy equipment. Temperature sensitivity during installation means watching the thermometer – they prefer 55 to 95°F.
Polyurethane systems reward patience with 15 to 25-year service lives and bulletproof UV resistance. Cure times stretch from 8 to 24 hours, but once cured, they handle -40°F to 200°F without breaking a sweat.
Polyaspartic coatings are the overachievers – same-day return to service with 20+ year lifespans. They work in temperatures from 35°F to 140°F. The premium chemistry commands premium pricing, but reduced downtime often justifies the investment.
MMA systems cure in 1 to 3 hours regardless of temperature. That speed and tolerance translates to 20+ year lifespans in high-traffic areas. Strong installation odors require serious ventilation planning.
Urethane cement provides 15 to 20 years of reliable service with best thermal shock resistance. These systems need 24 to 48 hours to cure and require skilled installation.
Specialty & Hybrid Systems
Novolac epoxy represents the premium tier of chemical resistance. Its tightly cross-linked molecular structure creates a barrier that outperforms standard epoxies when facing concentrated acids and bases.
Self-leveling formulations automatically smooth out surface imperfections while they cure, creating perfectly level surfaces without roller marks. Automotive showrooms and pharmaceutical manufacturing areas benefit from these systems.
Antimicrobial additives can be built into coating systems to provide ongoing protection against bacteria, mold, and mildew growth. Healthcare facilities and food processing plants benefit from this extra protection.
Decorative flake systems prove that performance and beauty can work together. Vinyl or quartz flakes create attractive, slip-resistant surfaces while helping hide minor surface imperfections and normal wear patterns.
How to Select the Perfect Coating for Your Facility
Choosing the right industrial floor coatings for your facility isn’t a one-size-fits-all decision. Your specific operating conditions, performance needs, and downtime constraints all play crucial roles in determining which coating system will serve you best for years to come.
Warehouse operations face unique challenges that make coating selection critical. With forklifts constantly moving heavy loads and pallets being dropped or dragged across surfaces, you need systems that can handle serious abuse. Epoxy or polyaspartic systems with 15-25 mil thickness provide the durability these environments demand while keeping costs reasonable. The key is finding that sweet spot between performance and budget.
Food processing facilities operate under an entirely different set of rules. USDA and FDA regulations require surfaces that are seamless, non-porous, and easy to sanitize completely. Add in the thermal shock from hot washdowns and aggressive cleaning chemicals, and you quickly see why urethane cement systems dominate these applications. They’re built to handle everything from boiling water to harsh sanitizers without breaking down.
Laboratory environments present their own puzzle. You’re dealing with sensitive electronic equipment that can be damaged by static electricity, plus various chemicals that could attack the wrong coating system. ESD-controlled coatings become essential, often paired with novolac epoxy chemistry for superior chemical resistance. It’s specialized work that requires specialized solutions.
Automotive facilities want the best of both worlds – showroom aesthetics combined with real-world durability. Oil spills, brake fluid, and constant foot traffic demand chemical resistance, while customers expect a polished, professional appearance. Polyaspartic systems with decorative flakes deliver both performance and visual appeal.

Performance Factors to Prioritize
Durability forms the foundation of any successful coating system. You want abrasion loss ratings below 10mg for high-traffic areas – anything higher and you’ll see premature wear patterns that look unprofessional and create maintenance headaches. Impact resistance matters just as much when tools get dropped or equipment gets moved around carelessly.
Chemical exposure analysis requires honest assessment of what your floors will encounter. Don’t just think about your primary processes – consider cleaning chemicals, accidental spills, and even what maintenance crews might track in. Different coating chemistries handle different chemical families better, so matching your specific exposure risks to the right system prevents costly failures down the road.
Slip coefficient requirements vary dramatically based on your application. Wet processing areas need textured surfaces for safety, while clean rooms might prioritize smooth finishes for easy sanitization. The good news is that anti-slip additives can be incorporated during installation to achieve exactly the traction level you need.
Thermal shock resistance becomes critical when your floors experience temperature swings. Food processing plants with hot washdowns, manufacturing facilities with heated processes, or even areas near loading docks where cold air rushes in during winter all need coatings that won’t crack or debond from thermal stress.
VOC compliance isn’t just about following regulations – it’s about creating healthier work environments for your team. Low-VOC formulations and water-based systems help facilities meet environmental objectives while contributing to green building certifications that can provide long-term value.
More info about Commercial Flooring
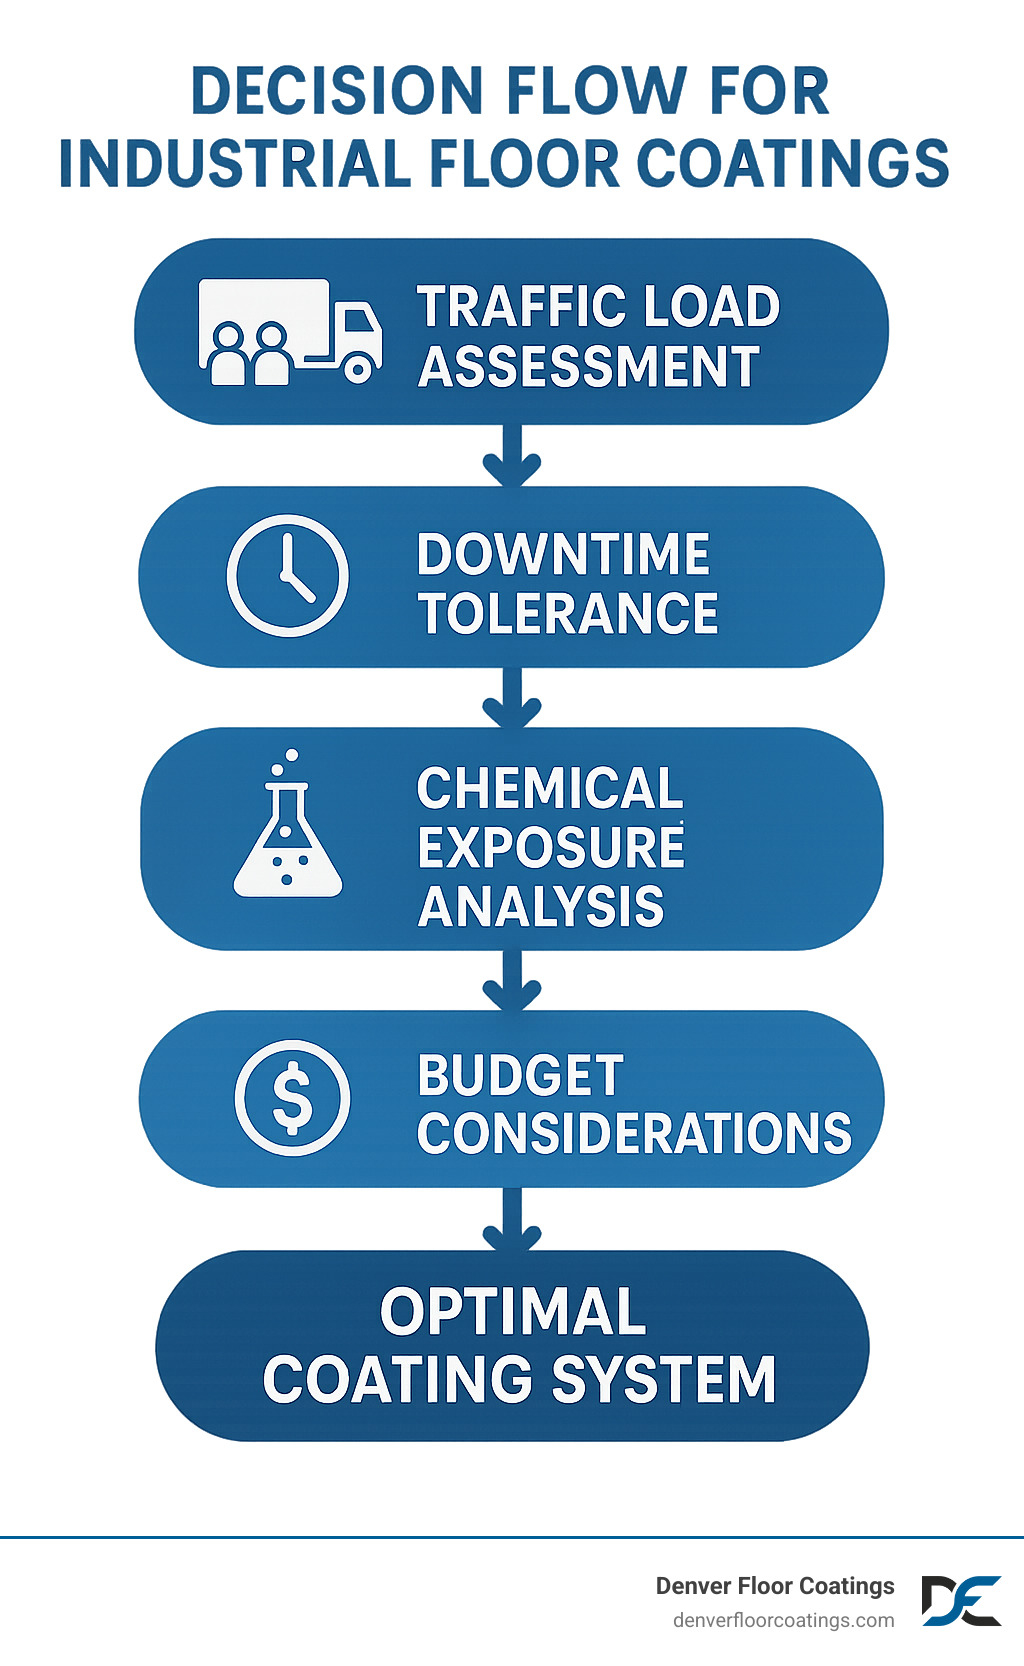
Decision Flow for Industrial Floor Coatings
Traffic load assessment starts with honest numbers. Light traffic areas seeing fewer than 25 people daily can often work with more economical acrylic or thin epoxy systems. But heavy traffic zones with constant forklift activity or manufacturing equipment need the robust protection of polyaspartic or MMA systems, even though they cost more upfront.
Return-to-service requirements often end up driving coating selection more than any performance factor. If your facility can’t afford multi-day shutdowns, fast-cure systems like polyaspartic or MMA become essential despite higher material costs. Sometimes paying more for speed saves money in lost production time.
Budget considerations should always include lifecycle costs, not just initial installation expenses. Premium systems with longer lifespans frequently provide better value over time, even with higher upfront investment. A coating that lasts 20 years instead of 10 essentially costs half as much per year of service.
Sustainability goals increasingly influence coating decisions in corporate environments. Bio-based resins, recycled content, and systems that contribute to LEED certification align with environmental objectives while often providing operational benefits like improved indoor air quality and worker satisfaction.
Installation & Life-Cycle Care Best Practices
Even the best industrial floor coatings will fail miserably if they’re not installed properly. Surface preparation isn’t just important, it’s absolutely critical to coating success.
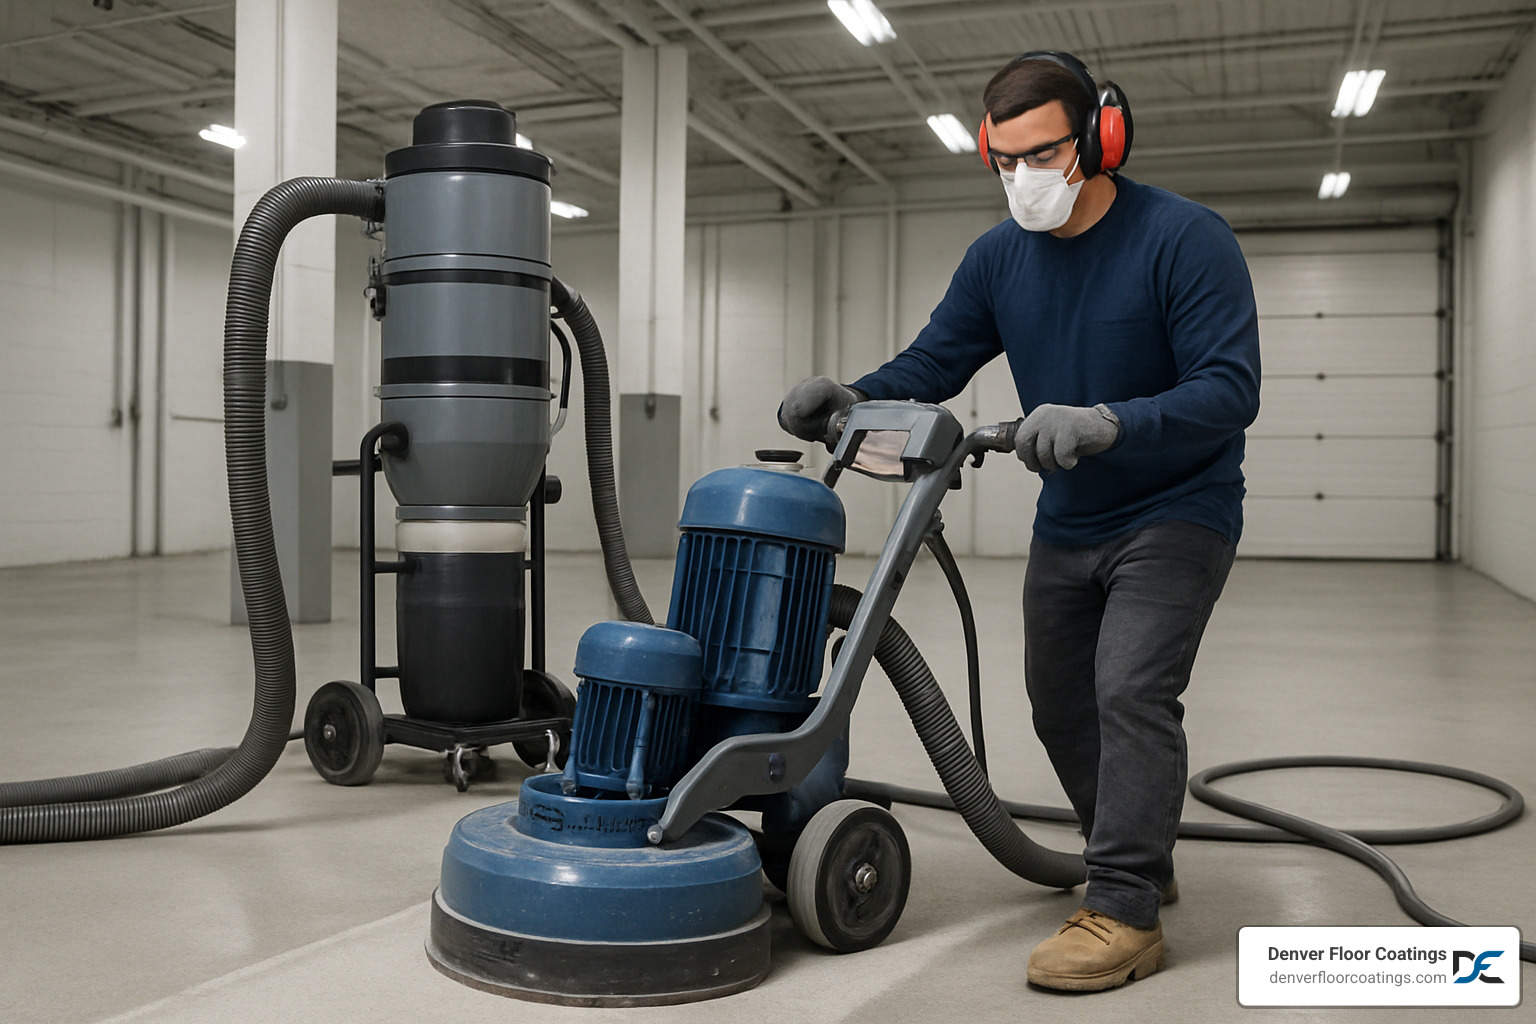
Mechanical profiling through diamond grinding or shotblasting creates the surface profile your coating needs to grab onto the concrete. This process removes contaminants, weak concrete, and creates the microscopic “teeth” that ensure proper adhesion.
Moisture mitigation addresses what I consider the silent killer of coating systems. Moisture vapor can push up from below, causing coatings to bubble, peel, and fail. Moisture testing should be mandatory on every project, with vapor barrier primers applied when moisture levels exceed the coating system’s tolerance.
Primer selection isn’t one-size-fits-all. Different substrates and conditions require specific primers. High-moisture primers work where standard primers would fail. Getting this wrong is like building a house on a shaky foundation.
The beauty of multi-coat build systems lies in their flexibility. Base coats handle adhesion and chemical resistance. Topcoats deliver wear resistance and aesthetics. This layered approach allows customization of thickness and performance characteristics.
Cure schedules can’t be rushed. Temperature, humidity, and ventilation all affect curing. I’ve seen facilities try to cut corners here, only to face premature failure and costly repairs.
Maintenance plans separate successful installations from eventual disasters. Regular cleaning with appropriate chemicals prevents contamination buildup. Periodic inspections catch small issues before they become big problems.
The most common failure causes are completely preventable: poor surface preparation, moisture-related adhesion loss, and UV degradation in inappropriate applications.
Extending Coating Longevity
Scheduled cleaning using pH-neutral cleaners and soft-bristle equipment prevents gradual buildup of contaminants that slowly degrade coating surfaces.
Touch-up topcoats offer a cost-effective way to refresh worn areas and extend overall system life. High-traffic zones often benefit from periodic topcoat renewal every 3-5 years rather than complete system replacement.
Slip-resistant additives may need periodic renewal in areas where foot traffic wears the texture smooth. These additives can often be incorporated into maintenance topcoats, restoring both protection and traction.
Quarterly inspections are your early warning system. Small cracks, worn spots, or developing issues are much easier and cheaper to address than major repairs. Early intervention prevents small problems from spreading throughout the system.
More info about Professional Epoxy Floor Installation
Frequently Asked Questions about Industrial Floor Coatings
When facility managers start exploring industrial floor coatings, they naturally have questions about costs, timelines, and environmental impact. Every facility is unique, and what works perfectly in one warehouse might be completely wrong for a food processing plant.
How much do industrial floor coatings cost over their life cycle?
Life-cycle economics depend heavily on three major factors that can swing costs dramatically.
Preparation variables often surprise facility managers. A brand-new concrete slab might need only basic diamond grinding. But that 70-year-old warehouse floor with oil stains and cracks? That requires extensive repairs, possibly even partial resurfacing.
Preparation costs can range from minimal on new construction to representing 80% of the total project budget on severely damaged floors. Moisture mitigation systems, crack repairs, and accessibility challenges all add complexity and cost.
Coat count affects both material expenses and labor time. A basic two-coat epoxy system keeps costs reasonable. But decorative systems with metallic effects might require four or more coats – base coat, color coat, broadcast layer, grout coat, and protective topcoat.
Decorative upgrades like quartz aggregates or custom colors increase material costs but often provide better long-term value through improved chemical resistance and better wear pattern concealment.
Focus on total cost of ownership rather than initial installation costs. A premium system that lasts 20 years costs less per year than a budget system requiring replacement every 5 years.
What surface preparation is absolutely necessary?
Proper surface preparation determines everything, and there are no shortcuts that actually work.
Mechanical profiling through diamond grinding or shotblasting isn’t optional. This process removes all surface contaminants, opens the concrete pore structure, and creates the specific surface profile that coating manufacturers require for warranty coverage.
Proper preparation typically represents 60-70% of total project costs. It seems expensive until you consider that shortcuts almost always result in premature coating failure and complete system replacement.
Crack repair prevents coating systems from failing at stress concentration points. Hairline cracks can usually be filled with flexible epoxy compounds, but structural cracks require engineering evaluation.
Are there eco-friendly or low-VOC industrial floor coatings?
Environmental considerations have become increasingly important as facilities focus on indoor air quality and sustainability goals.
Water-based epoxy systems dramatically reduce VOC emissions compared to traditional solvent-based coatings. These systems support healthier indoor environments while providing excellent chemical resistance and durability.
Bio-based resins represent emerging technology that incorporates renewable plant-based materials rather than relying entirely on petroleum-derived components.
Regulatory credits for low-VOC systems can contribute toward LEED certification and other green building programs, sometimes offsetting the slightly higher costs while supporting corporate sustainability initiatives.
Indoor air quality benefits extend beyond regulatory compliance. Employees working in facilities with low-VOC coatings report fewer headaches and respiratory irritation commonly associated with chemical emissions.
Conclusion

Your facility’s floor is the foundation of everything that happens above it. When you understand that industrial floor coatings can be up to 80 times thicker than regular floor paint, it becomes clear why these systems provide such dramatic improvements in durability and performance.
The change we see in facilities is remarkable. A food processing plant that struggled with sanitation suddenly has seamless surfaces that clean effortlessly. A warehouse plagued by concrete dust and cracking floors becomes a clean, professional environment where forklifts glide smoothly and workers feel proud of their workspace.
The benefits we’ve covered – chemical resistance, impact protection, easy maintenance, and regulatory compliance – aren’t just technical specifications. They translate into real-world advantages like reduced downtime, lower maintenance costs, improved safety, and facilities that actually look professional.
During my years at 3M, I learned that the best engineering solutions are the ones that solve multiple problems at once. That’s exactly what the right coating system does. It protects your concrete investment while creating safer work environments and supporting your operational goals.
The key is choosing the system that matches your specific needs. Whether you’re dealing with heavy forklift traffic, chemical spills, thermal shock from washdowns, or the need for electrostatic discharge protection, there’s a coating chemistry designed for your situation.
Don’t let your concrete floors limit your facility’s potential. The investment in proper industrial floor coatings pays for itself through extended floor life, reduced maintenance, improved safety, and the professional appearance that reflects well on your entire operation.